Table of Contents
- What Spout Pouch Torque Testing Measures
- Application Torque vs. Removal Torque
- How to Build a Pouch Cap Torque Specification
- Torque Test Equipment and Fixtures
- Recommended Torque Test Procedure
- Variables That Change Torque Results
- Testing Tamper-Evident Cap Torque
- How to Interpret Torque Test Results
- Production Sampling and Buyer Documentation
Spout pouch torque testing verifies that threaded caps are applied tightly enough to support closure integrity but remain practical for users to open. This guide explains application torque, removal torque, tamper-evident bridge break behavior, test equipment, procedures, specifications, and production controls.
What Spout Pouch Torque Testing Measures
Spout pouch torque testing measures the rotational force used to tighten a threaded cap and the force later required to open it. The objective is to establish a validated operating window: the cap must engage the spout correctly and maintain the intended seal while remaining suitable for the target user to remove. There is no universal torque value for all pouches. The correct limits depend on the cap and spout geometry, thread design, sealing mechanism, tamper-evident features, materials, filling process, product, and expected storage conditions.
Torque is commonly reported in newton-centimeters (N-cm), newton-meters (N-m), or pound-force inches (lbf-in). A specification should use one primary unit and state any conversion method. It should also distinguish measurements taken during application from measurements taken during opening.
Torque testing is one part of a broader closure validation program. It does not replace leak, seal, drop, distribution, or product-compatibility testing. Buyers should evaluate the cap, fitment, pouch body, and filling operation as one packaging system. The available guide to spout pouch caps and fitments explains how closure geometry and dispensing requirements affect fitment selection.
Application Torque vs. Removal Torque
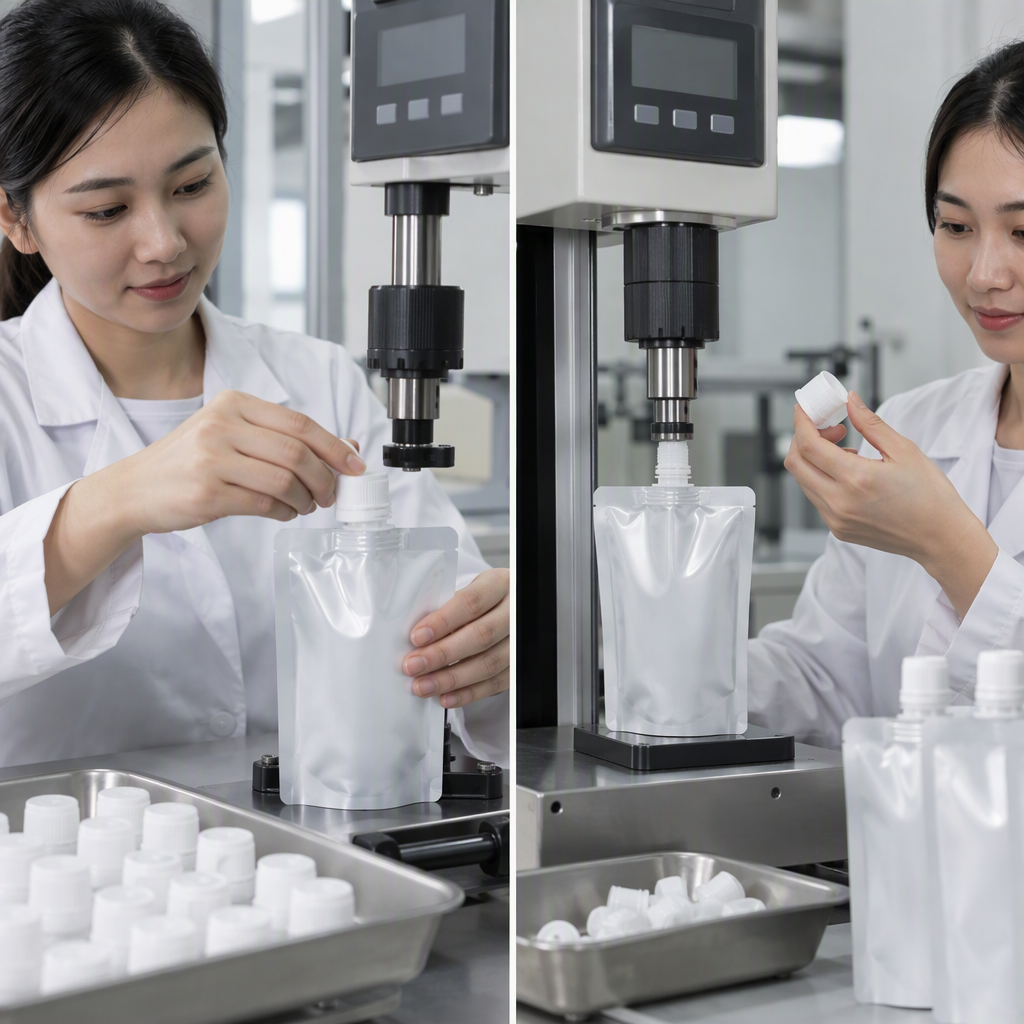
Application and removal torque answer different quality questions and should not be treated as interchangeable values.
| Measurement | What it indicates | When it is measured | Typical concern |
|---|---|---|---|
| Cap application torque | Rotational force delivered while tightening the cap onto the spout | During controlled laboratory capping or on the filling line | Under-application, over-application, crossed threads, or variable capper output |
| Immediate removal torque | Force needed to begin opening soon after application | After a defined short dwell period | Confirmation of initial closure response |
| Aged removal torque | Opening force after a defined conditioning or storage interval | After hours, days, or a validated aging period | Torque loss, excessive tightening, material relaxation, or product effects |
| Running torque | Force required to continue turning after initial movement | Across the opening rotation | Thread interference, distortion, or inconsistent opening feel |
Removal torque is not expected to equal application torque. Plastic stress relaxation, thread friction, sealing surface compression, temperature, elapsed time, and cap construction can change the measured opening force. Consequently, buyers should not set removal limits by applying an arbitrary percentage to the cap application torque. Limits should come from tests on representative caps, spouts, filled pouches, and process conditions.
How to Build a Pouch Cap Torque Specification
A usable pouch cap torque specification defines the complete test condition, not only a nominal number. Start with the exact cap and spout part numbers, including resin, color masterbatch where relevant, thread geometry, orifice size, tamper-evident design, plug seal, liner, and any induction or membrane seal. Similar-looking closures may not produce equivalent results.
The document should state:
- Target application torque plus acceptable lower and upper limits
- Immediate and aged removal torque limits, if both are required
- Separate tamper-evident bridge break or band release requirements where measurable
- Torque unit, instrument range, resolution, calibration status, and rotation speed
- Fixture design and how the flexible pouch or fitment is restrained
- Cap application method, including manual, laboratory-controlled, or production capper
- Dwell time between application and removal tests
- Sample conditioning temperature, duration, orientation, and fill condition
- Sample size, test frequency, acceptance rule, and treatment of invalid tests
Develop preliminary limits through trials across expected manufacturing conditions. Include normal component tolerances and representative production-line settings. Final limits should correlate with closure integrity and opening usability rather than reflecting only what a single laboratory sample achieved. Where hot filling is used, the validation plan should account for the fitment and closure behavior described in this hot-fill spout pouch engineering guide.
Torque Test Equipment and Fixtures
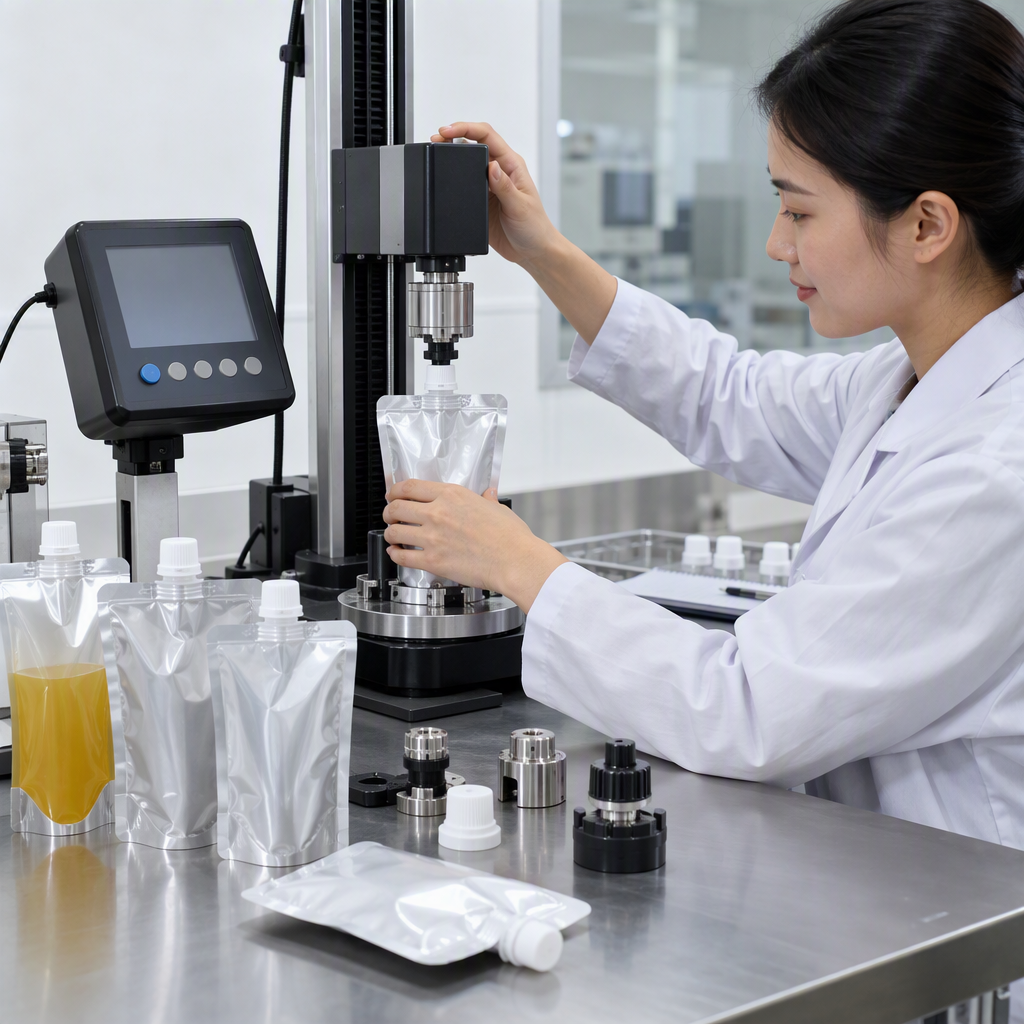
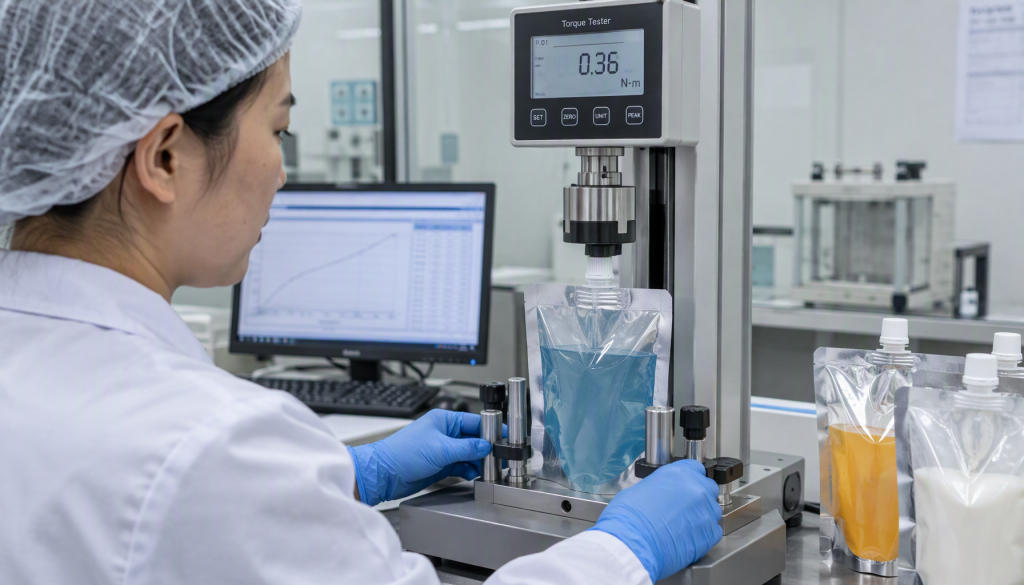
The instrument and fixture must match the expected torque range and the flexible format of the package. A pouch cannot always be clamped like a rigid bottle because excessive fixture pressure may distort the fitment neck or pouch seals.
| Equipment or component | Purpose | Selection factors |
|---|---|---|
| Digital torque analyzer | Measures peak and, on suitable models, continuous torque during opening or closing | Measurement range, resolution, accuracy, sampling rate, rotation control, and data export |
| Motorized torque stand | Applies controlled speed and direction | Repeatability, programmable angle, speed range, and peak detection |
| Cap chuck | Grips the cap without slipping | Cap diameter, rib pattern, closure shape, and risk of cap deformation |
| Spout or pouch fixture | Prevents the fitment from rotating during testing | Fitment flange geometry, pouch orientation, restraint consistency, and access to the cap |
| Production torque transducer | Checks capper output or application behavior on the line | Compatibility with the capping head, line speed, and measurement method |
| Calibration device or service | Confirms instrument response against traceable reference equipment | Required interval, torque direction, expected range, and documentation |
A hand-held torque gauge may be useful for troubleshooting, but operator speed, grip, and alignment can increase variation. A motorized system is preferable when a controlled rotation rate or a full torque-angle curve is required. Regardless of equipment type, conduct a fixture repeatability study before using the method for acceptance decisions.
Recommended Torque Test Procedure
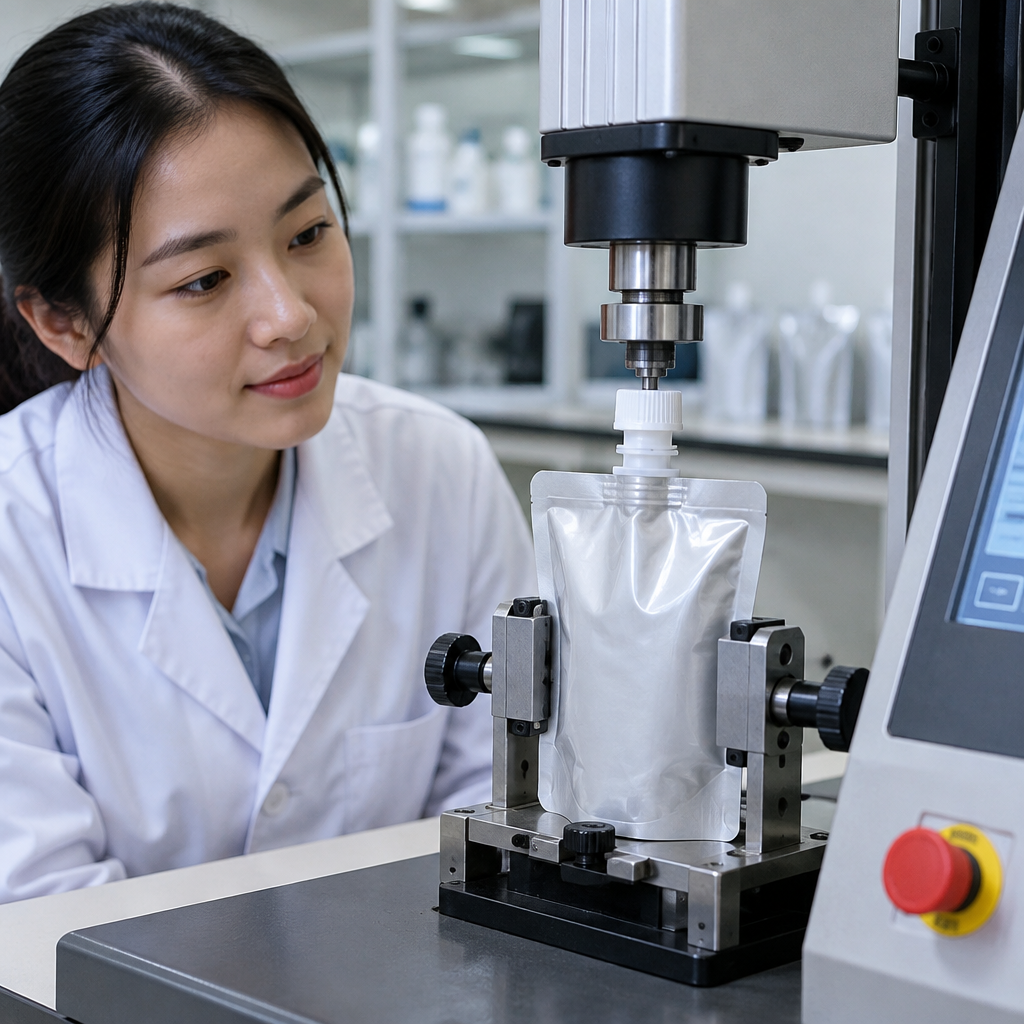
The following sequence provides a practical starting framework. The buyer and supplier should convert it into a controlled procedure for the selected package.
- Identify samples. Record the pouch, spout, cap, molding lot, pouch production lot, filling condition, and test date.
- Inspect components. Exclude and document visibly damaged samples. Do not silently replace failures caused by crossed threads, incomplete molding, or fitment distortion.
- Condition samples. Hold them for the specified time and temperature. Keep orientation and fill level consistent.
- Verify the instrument. Confirm calibration status, zero the analyzer, install the specified fixture, and check the measurement direction.
- Apply the cap. Use the defined capping equipment, chuck, speed, and target application torque. Avoid hand application unless the approved method specifically requires it.
- Wait for the specified dwell. Measure immediate removal torque only after the documented interval. Use separately capped samples for later intervals when opening is destructive.
- Measure removal. Align the spout, restrain the pouch without distorting it, rotate at the specified speed, and record the required peaks or torque-angle curve.
- Inspect after opening. Check threads, plug seals, tamper bands, bridges, spout necks, and evidence of cap or fitment damage.
- Report all valid results. Record individual readings, summary statistics, test conditions, abnormalities, and disposition against the approved limits.
ASTM closure torque methods may provide useful terminology or procedural concepts, but their applicability to a particular flexible pouch and fitment must be reviewed. A method developed for rigid containers should not be adopted without confirming that pouch restraint and fitment deformation are controlled.
Variables That Change Torque Results
Torque variation can originate in the closure components, capping process, product, environment, or measurement system. Important variables include cap and spout molding tolerances, thread finish, resin stiffness, cap rib geometry, plug-seal interference, tamper-band construction, and lubricant or product residue on the threads.
Process conditions also matter. Capper chuck wear, spindle speed, applied top load, misalignment, cap feeding, pouch support, and line speed can change application behavior. A cap that appears acceptable during slow laboratory application may respond differently on a production capper. Trials should therefore include the intended equipment or a method that reasonably represents it.
Temperature and elapsed time affect plastic components. Hot filling may temporarily soften a fitment or closure, while cooling and material relaxation may change removal torque. Cold storage can alter stiffness. Product oils, flavors, solvents, cleaners, or particulates may affect friction or polymer compatibility, depending on the formulation and contact path. These effects should be evaluated using the actual product or an appropriately justified simulant.
Torque results should also be reviewed alongside leakage and visible closure defects. A low reading may indicate an under-applied cap, stripped thread, dimensional mismatch, or measurement slip. A high reading may indicate excessive application, thread interference, contamination, or fitment deformation. The spout pouch defect identification guide provides additional context for investigating closure-related observations.
Testing Tamper-Evident Cap Torque
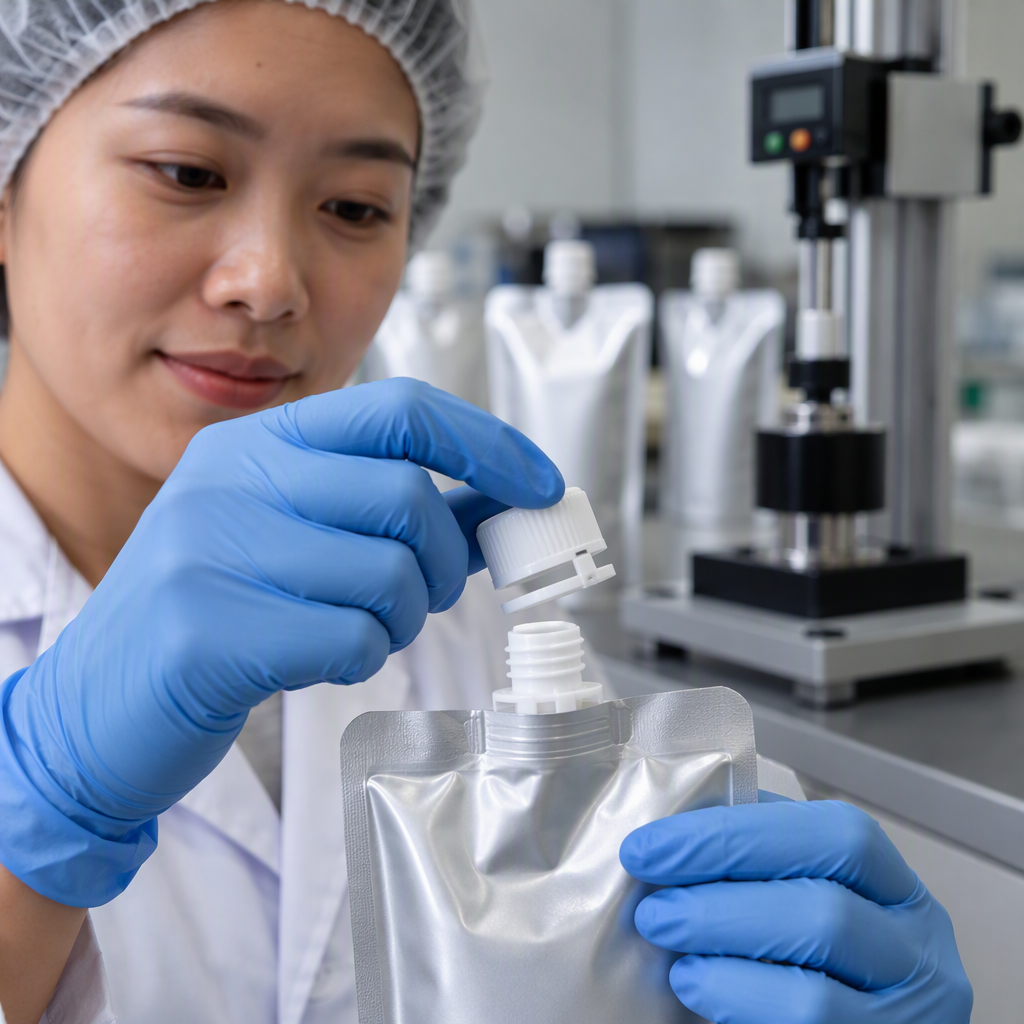
Tamper evident cap torque testing may produce more than one event on the opening curve. The initial peak can represent static thread friction, plug-seal release, tamper-band bridge break, or a combination of these events. A later peak may occur when the band passes a retaining feature or when the plug seal disengages. Visual inspection is needed to connect the recorded curve with the physical opening sequence.
For a tamper-evident closure, record the relevant characteristics separately where the equipment permits:
- Peak torque at first movement
- Torque or angle at bridge break
- Running torque after initial release
- Condition of every bridge after opening
- Whether the band remains on the fitment or follows the cap, according to its design
- Evidence of premature bridge damage before testing
A high total removal peak does not necessarily mean that the tamper-evident feature is strong, because thread friction or plug-seal interference may account for much of the load. Similarly, a cap can meet an overall removal torque limit while some bridges are already damaged. Combine instrument data with visual inspection and, when relevant, controlled opening-angle data.
Child-resistant closures require separate protocol-based testing and should not be qualified through torque measurements alone. Tamper evidence, child resistance, and ordinary opening usability are different performance questions.
How to Interpret Torque Test Results
Do not evaluate only the sample average. Individual readings, range, time trend, component lot, capping head, and failure mode provide the information needed to diagnose a process. Capability statistics can be useful after the measurement system is shown to be repeatable and the process is stable, but they should not conceal out-of-specification units.
| Observed pattern | Possible causes to investigate | Practical follow-up |
|---|---|---|
| Low application and low removal torque | Low capper setting, chuck slip, poor engagement, or incorrect cap | Verify settings, chuck condition, component identity, and thread engagement |
| Target application but low aged removal torque | Material relaxation, temperature effect, contamination, or sealing-surface change | Repeat at defined intervals and inspect the cap-spout interface |
| High removal torque | Over-application, thread interference, excessive plug-seal fit, or product residue | Inspect components and correlate readings with application settings |
| Wide variation within one lot | Fixture inconsistency, capper head variation, molding tolerance, or misalignment | Check the measurement system and separate results by cavity or capping head |
| Normal torque with leakage | Seal geometry, component damage, spout weld, or product-path issue | Perform leak testing and inspect the complete closure and pouch assembly |
Torque conformity alone does not prove package integrity. Results should be assessed within the wider spout pouch quality control program, including fitment sealing, pouch seals, visual condition, dimensions, and application-specific performance tests.
Production Sampling and Buyer Documentation
Once validation establishes the torque window, translate it into controls for incoming components, pouch conversion, filling, capping, and finished-package inspection. Responsibility must be explicit: a pouch converter may supply the pouch with an inserted fitment, while the buyer or contract filler applies the cap after filling. In that arrangement, application torque is primarily controlled at the filling site, but fitment and cap dimensions remain part of supplier control.
A production plan can define start-up checks, checks after capper adjustment or component change, periodic checks by time or quantity, and end-of-run verification. Multi-head cappers should be sampled by head where traceability permits. Record component lots and equipment settings so an adverse trend can be isolated.
For shipment acceptance, identify whether torque is a critical, major, or other agreed defect category and specify the sampling rule. An AQL plan determines how many finished units are inspected and how a lot is accepted; it does not establish the engineering torque limits. See the spout pouch AQL sampling guide for the distinction between specification limits and lot acceptance.
Buyer documentation should include the approved cap and spout drawings, torque test procedure, current specification revision, instrument identification, calibration status, raw test results, lot information, deviations, and corrective actions. Torque records can also be incorporated into a broader pre-shipment spout pouch inspection checklist.
Before approving production, confirm the actual product, filling temperature, capper type, expected distribution environment, opening audience, and storage interval. These assumptions determine whether the laboratory method represents commercial use.
FAQ
What is spout pouch torque testing?
Spout pouch torque testing measures rotational force during cap tightening and opening. It is used to control cap application, verify removal behavior, evaluate torque retention, and investigate tamper-evident closure events. The method must identify the cap, spout, fixture, equipment, speed, dwell time, conditioning, and torque limits.
Is there a standard cap application torque for every spout pouch?
No. A suitable cap application torque depends on the matched cap and spout design, materials, sealing mechanism, capping equipment, product, filling conditions, and opening requirements. The closure supplier’s guidance can be a starting point, but the final range should be validated on the complete package.
Why is cap removal torque lower than application torque?
Removal torque often differs because plastic components relax after capping and because static friction, sealing-surface compression, temperature, and storage time change. It is not appropriate to assume a fixed application-to-removal ratio without package-specific test data.
When should removal torque be measured?
Measure it at documented intervals relevant to the packaging system. A program may include an immediate reading after a defined dwell, a later laboratory reading, and readings after conditioning, transportation simulation, or shelf-life intervals. Separate samples are normally required because opening is destructive.
Can torque testing confirm that a spout pouch will not leak?
No. Torque data can reveal some closure application problems, but it does not directly verify every leak path. Closure torque testing should be combined with appropriate leak testing, fitment-seal inspection, pouch-seal evaluation, and distribution testing.
How should a tamper-evident cap be evaluated?
Measure relevant opening peaks or the torque-angle curve and visually inspect the band and bridges before and after opening. Overall removal torque alone may not show whether the bridges were intact or when they broke. The approved method should define the intended band behavior and rejection criteria.
Should empty and filled pouches produce the same torque results?
Not necessarily. Product residue, internal pressure, filling temperature, cooling, pouch handling, and storage orientation can affect closure behavior. Development work may begin with empty samples, but final validation should use representative filled packages or a justified equivalent condition.
Discuss Your Spout Pouch Closure Requirements
Contact HUACANG Packaging to review your pouch structure, spout fitment, cap and tamper-evident requirements, artwork, MOQ, sample plan, filling conditions, and quotation details.